PLC-Controlled 3D-Filament Pellet Sorting Workstation
Project Overview
This project automated an SMC HAS-200 workstation for 3D-filament pellet sorting. A Rockwell PLC coordinated the magazine, conveyor, pneumatic handling, vacuum pick-and-place, barcode validation, accept/reject logic, and operator controls.
PLC project files · Automatic mode video · Manual mode video
Control System at a Glance
| System | Implementation |
|---|---|
| PLC | Rockwell PLC programmed in Studio 5000 Logix Designer |
| Programming | Ladder logic with modular routines |
| Material handling | Magazine index, conveyor, pneumatic cylinders, and vacuum pickup |
| Identification | Barcode reader with transfer-ID validation |
| Sorting | Accept/reject decision with reject-cylinder actuation |
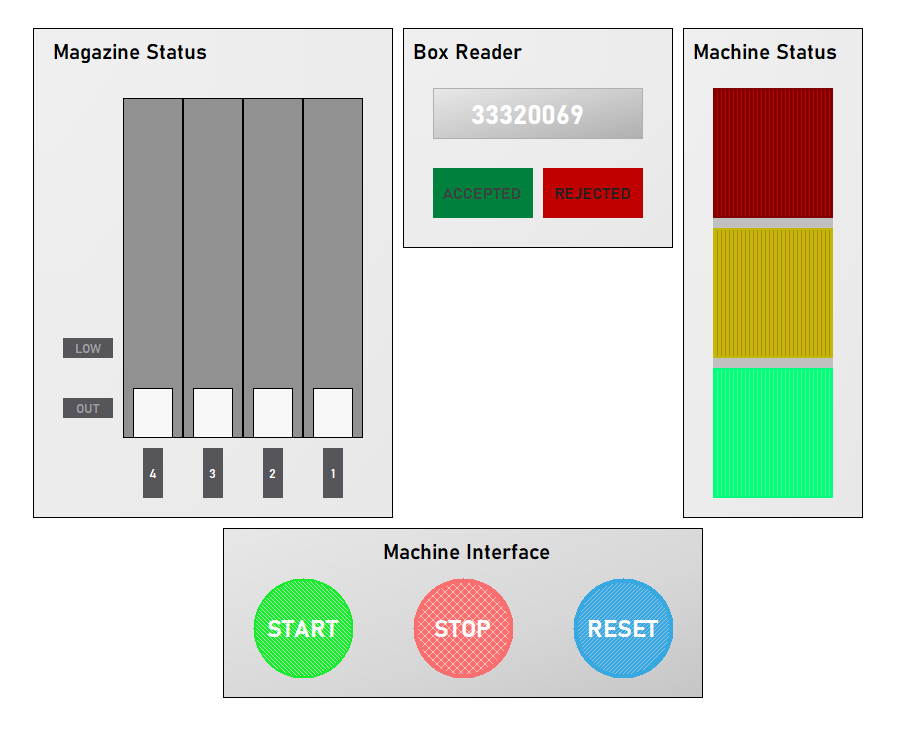
| Operator interface | HMI/SCADA start, stop, reset, automatic, and manual controls |
| Safety and recovery | Interlocks, sensor checks, timers, stop logic, and machine reset |
| Status feedback | Tower lights and HMI machine-state feedback |
PLC Routines
- AA Main Routine: Coordinates the machine sequence and calls the control routines.
- Production: Runs the automatic pick, transfer, release, and magazine-index cycle.
- Barcode Reader: Validates the scanned identifier and extracts sorting data.
- Accept Reject Box: Controls the reject cylinder for nonconforming boxes.
- Magazine Index: Advances the next box into position.
- Machine Reset: Returns the workstation to a known start state.
- Stop: Handles operator and fault stops.
- Flasher Timers: Controls timed status and tower-light behavior.
My Contributions
- Developed and debugged modular ladder-logic routines for the complete workstation sequence.
- Integrated barcode data, sensors, pneumatic actuators, conveyor motion, and vacuum handling.
- Built HMI/SCADA controls for automatic and manual operation.
- Implemented interlocks, timers, sensor verification, stop handling, and reset recovery.
Results
The completed control system demonstrated automatic and manual workstation operation, barcode-based sorting, coordinated pneumatic handling, and operator-visible machine status through the HMI/SCADA interface.